Our steam system solutions are built on the broadest product portfolio, covering almost every aspect of steam and fluid processing. With such a wide range we can match the right equipment to your needs, working together seamlessly while keeping operating costs to a minimum. We also back it with leading industry warranties, including lifetime material warranties on selected products and extended warranty options.
To improve plant efficiency and save energy, condensate, air and other non-condensable gases must be drained from the steam system without losing live steam - and the condensate recovered. Our steam traps cover every application, with performance monitoring to complete the range.
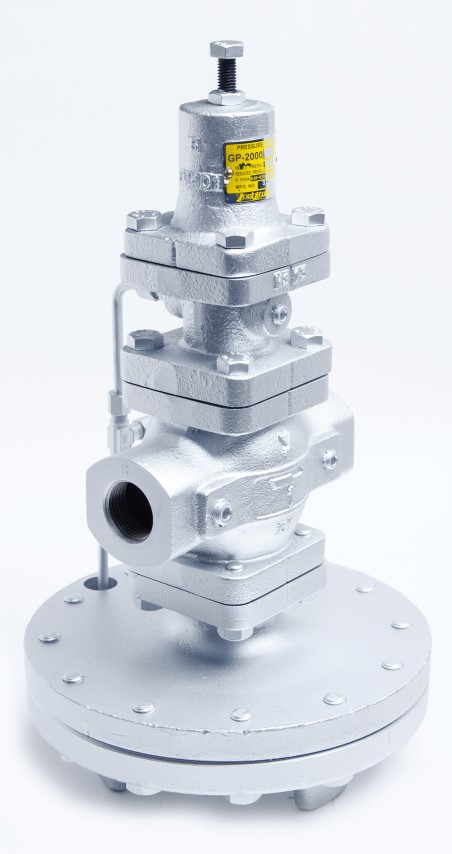
Control valves, electric and pneumatic actuators, positioners, pressure reducing and safety valves for accurate regulation and protection of steam and process systems.
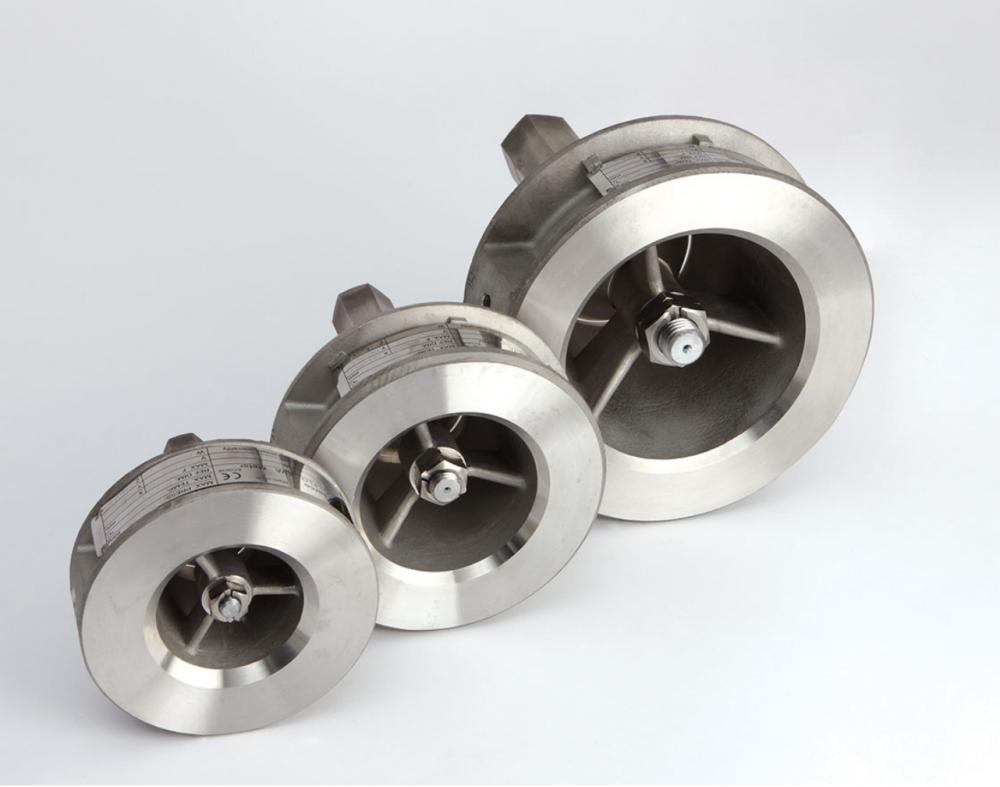
For steam equipment to be efficient, safe, reliable and long-lived, the steam must be clean and dry and the system easy to maintain. We offer a complete range of pipeline ancillaries.
A wide range of boiler control systems - whether installing a complete new boilerhouse or replacing a single blowdown valve.
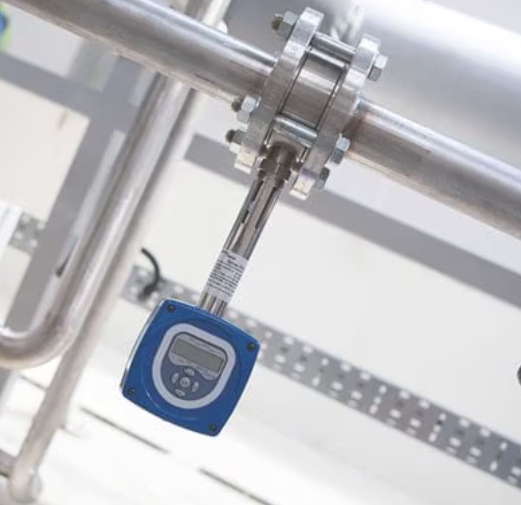
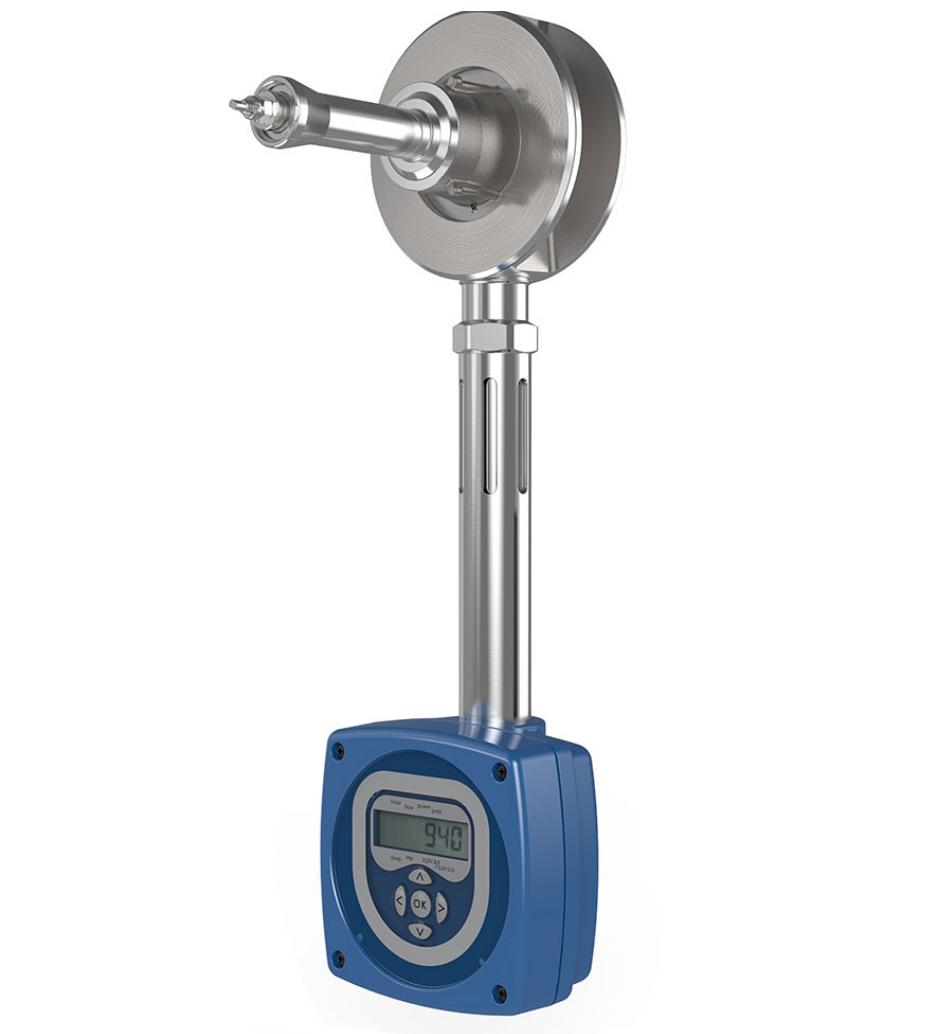
Whatever your process or system, there is a Spirax Sarco flowmeter for the job - accurate, reliable and versatile for steam, liquids and gases, with displays and transmitters for energy management.
To maximise energy efficiency, recovering condensate back to the boilerhouse is critical. Our condensate recovery equipment does this efficiently and economically.
Ensure compressed air reaches the point of use at the right flow and quality, and add direct steam injection humidifiers for precise humidity control.
We supply well-engineered packaged heat exchange units so you can focus on your core business - from design and manufacturing through to a complete package.
Many industries use clean steam to reduce the risk of product or process contamination. We supply clean steam generators and valves for hygienic duty.